
Quality & Certification
Top 5%
Uster Standard Quality
100%
Computerized Lab Testing
Zero Defect
Contamination Policy
Global
Accredited Certifications
Certifications
Quality Backed by Global Standards
Our operations adhere to internationally accredited certifications, ensuring traceability, sustainable farming support, and superior product integrity across our supply chain.
 Quality Control
World-Class Testing Laboratory
Our state-of-the-art QC department operates fully computerized testing instruments under climate-controlled ISO conditions to guarantee consistency and strength.
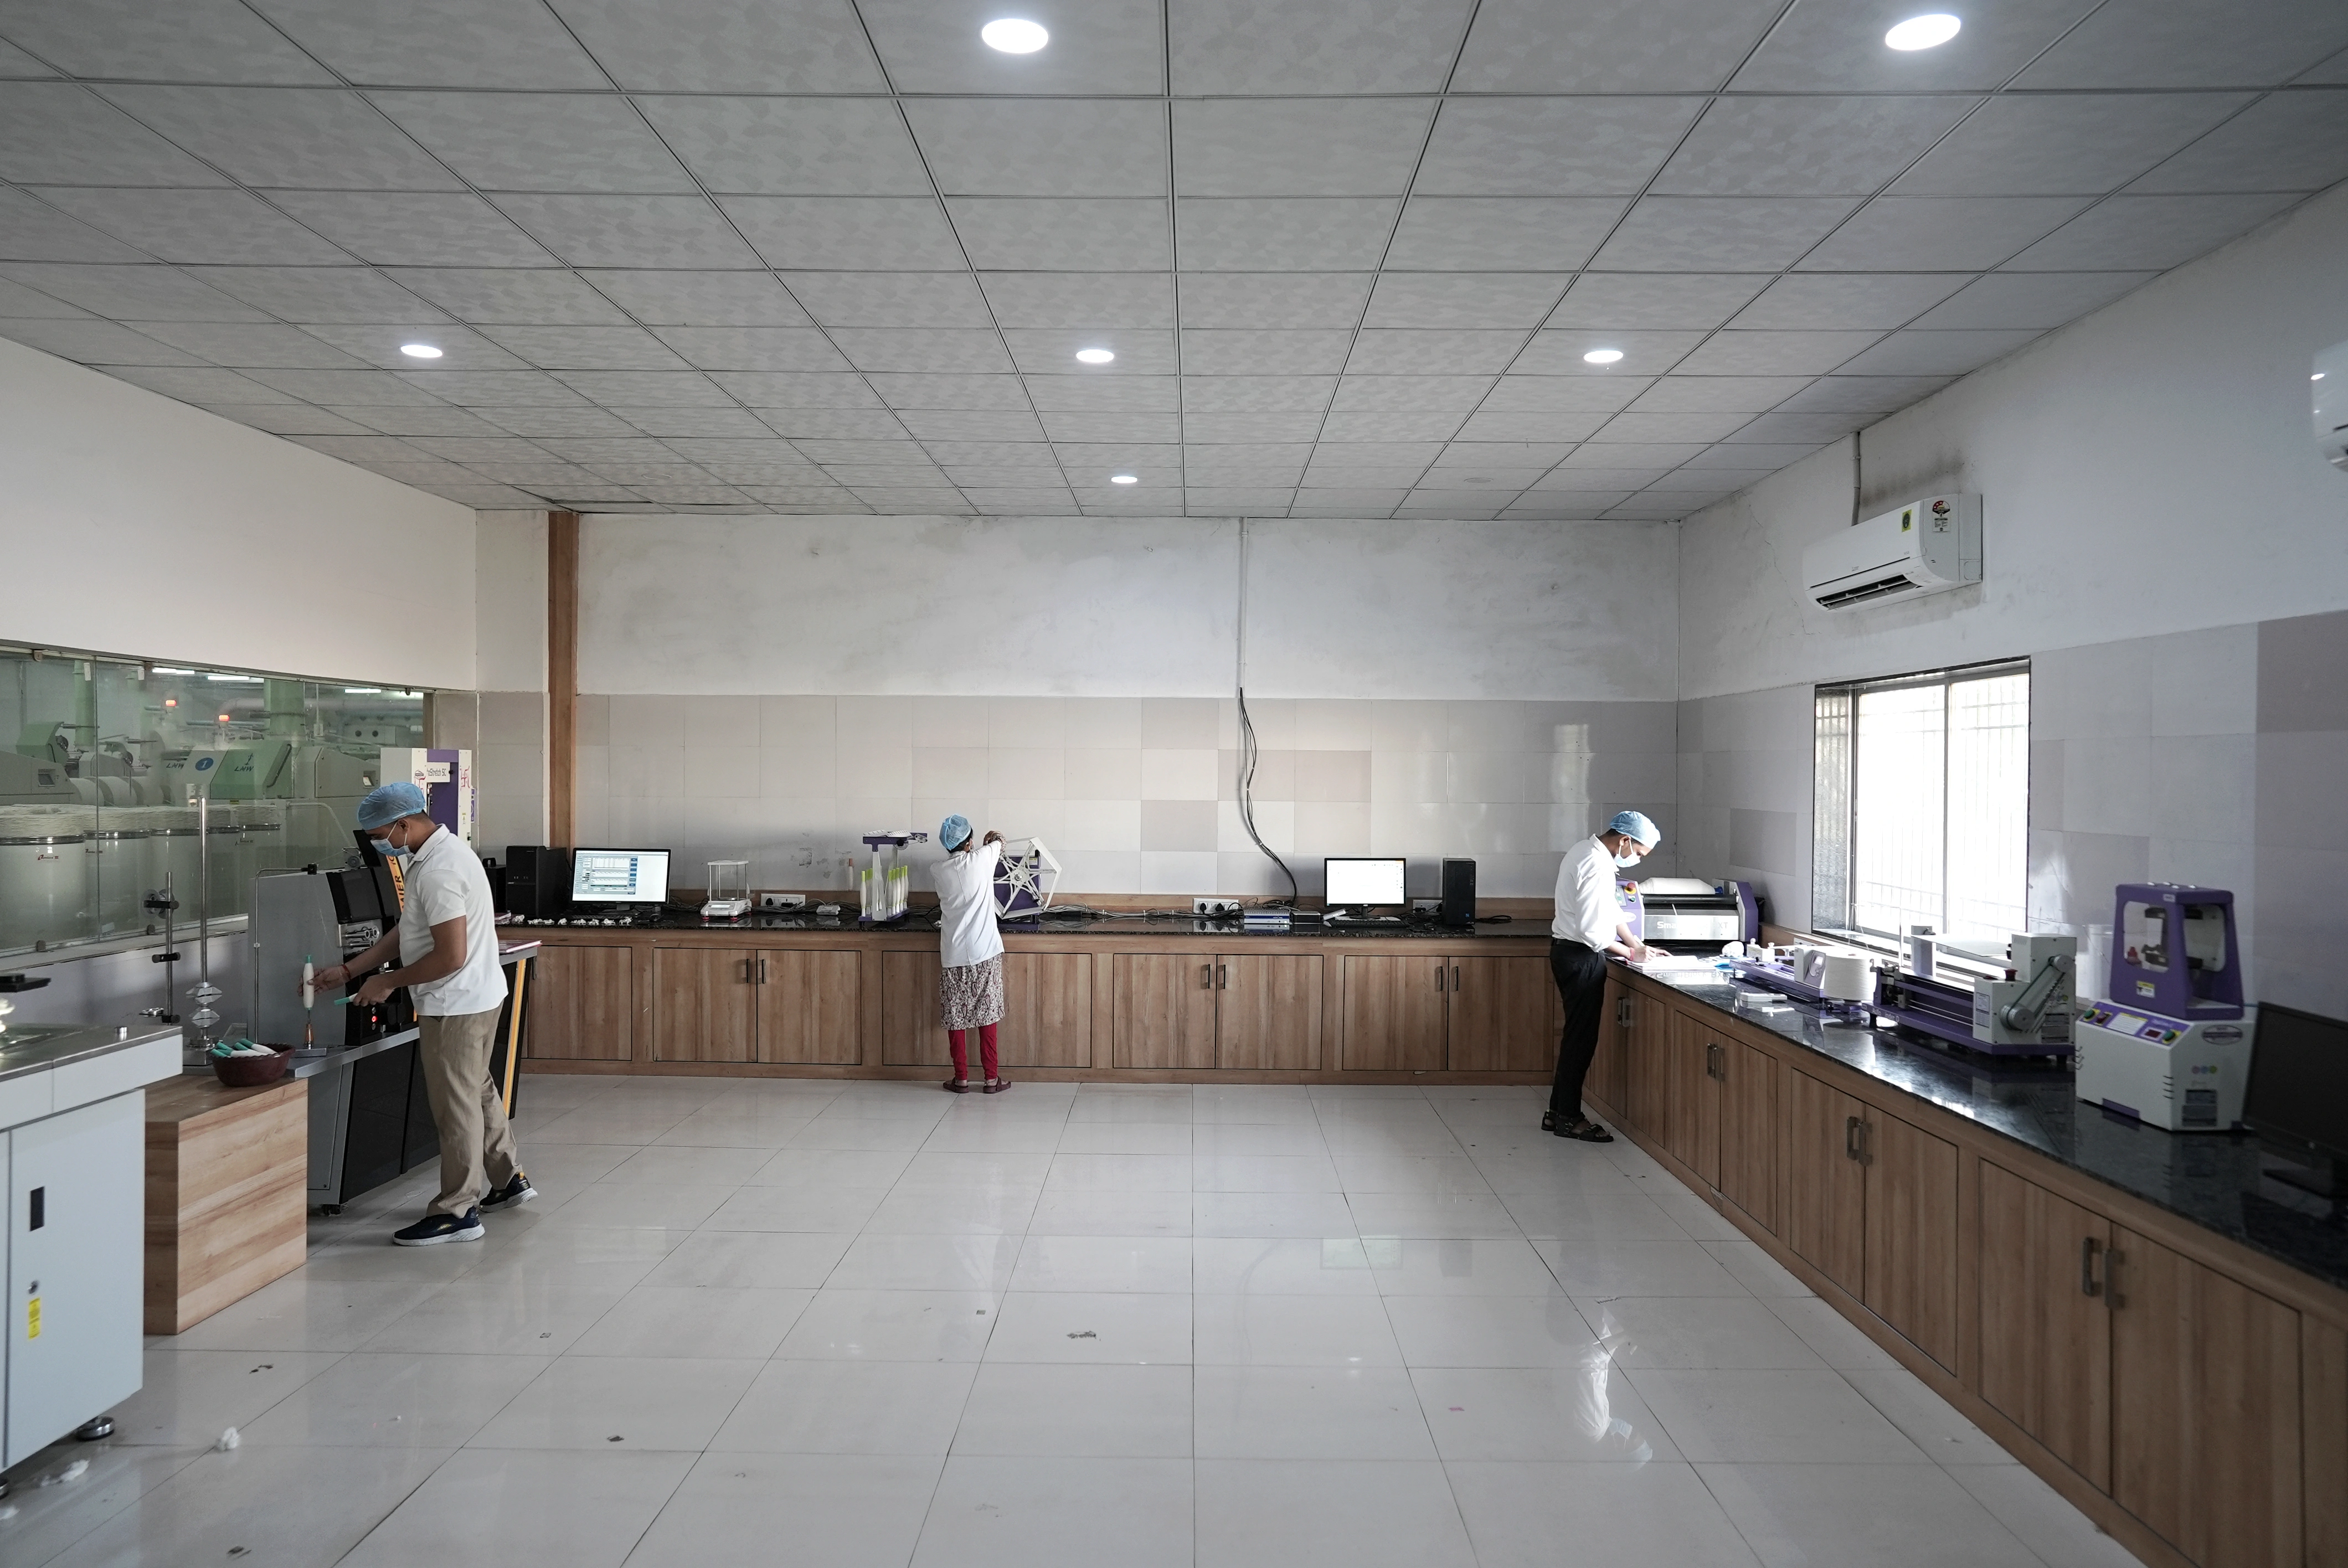
Climate-Controlled Lab
Continuous temperature (20°C ± 2°C) and relative humidity (65% ± 2% RH) control ensuring consistent moisture regain.
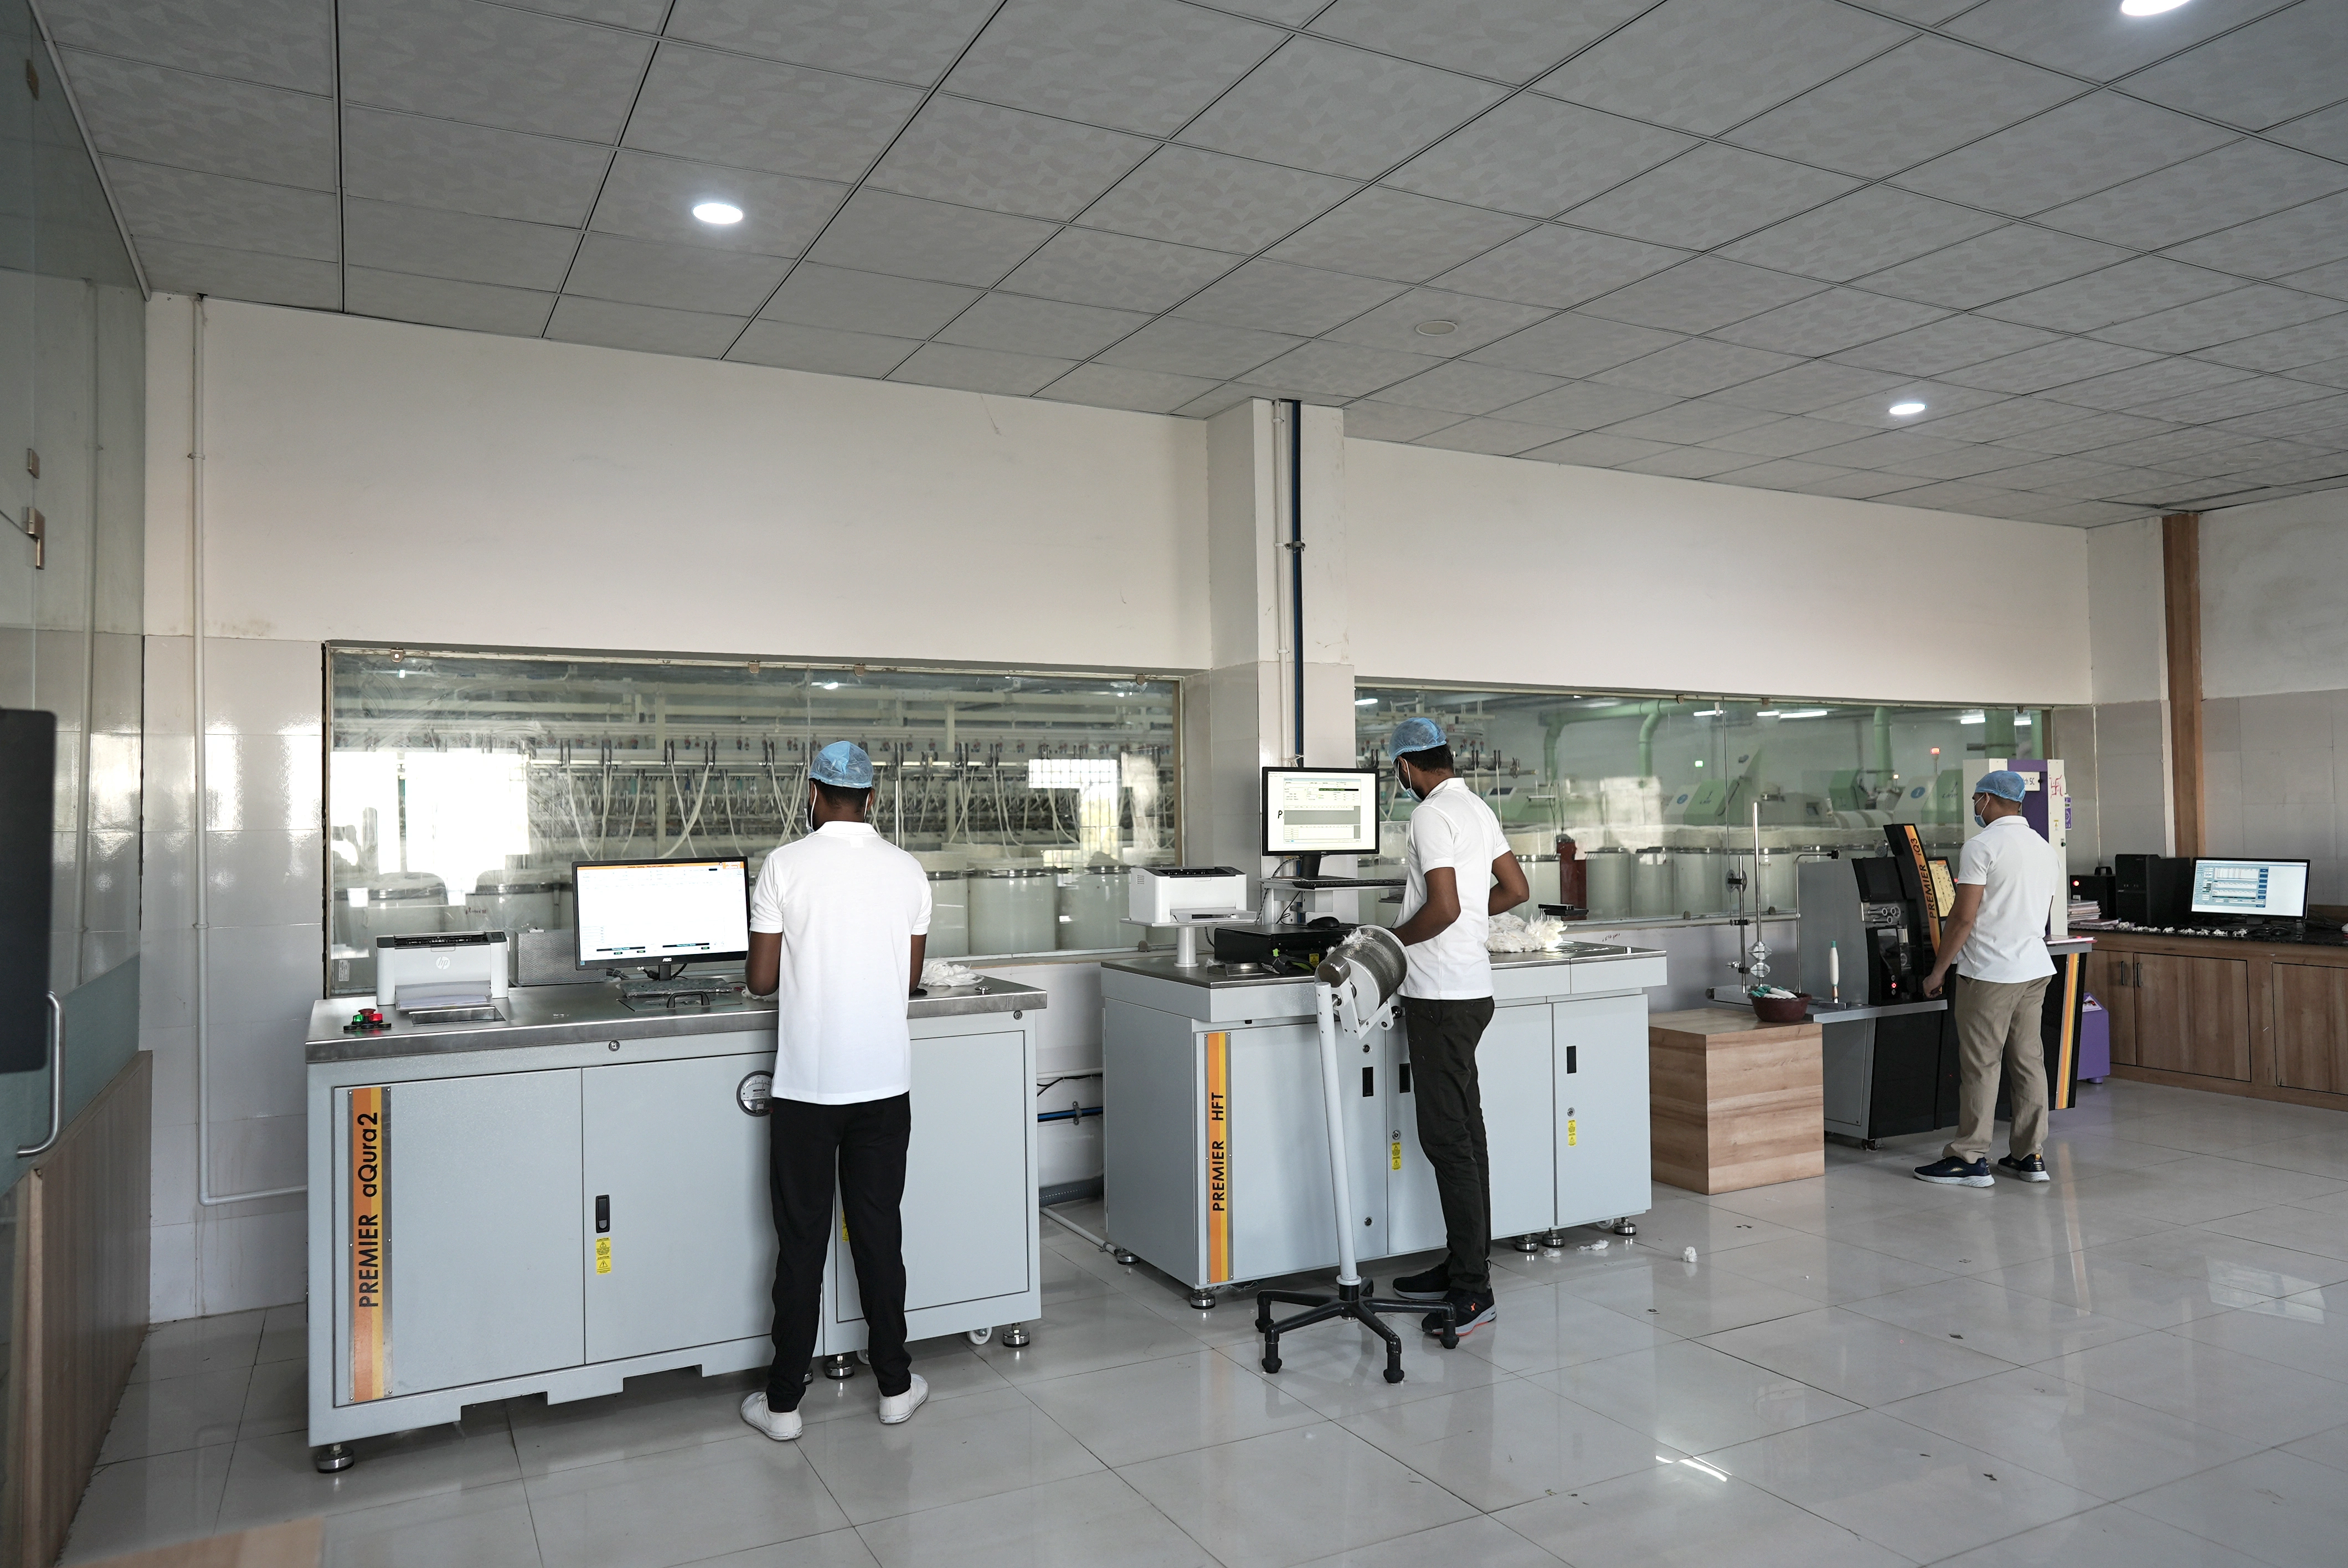
Premier iQ3 & Fibre Control
Evaluates mass variation and imperfections using high-precision capacitive sensors for flawless knitting & weaving.
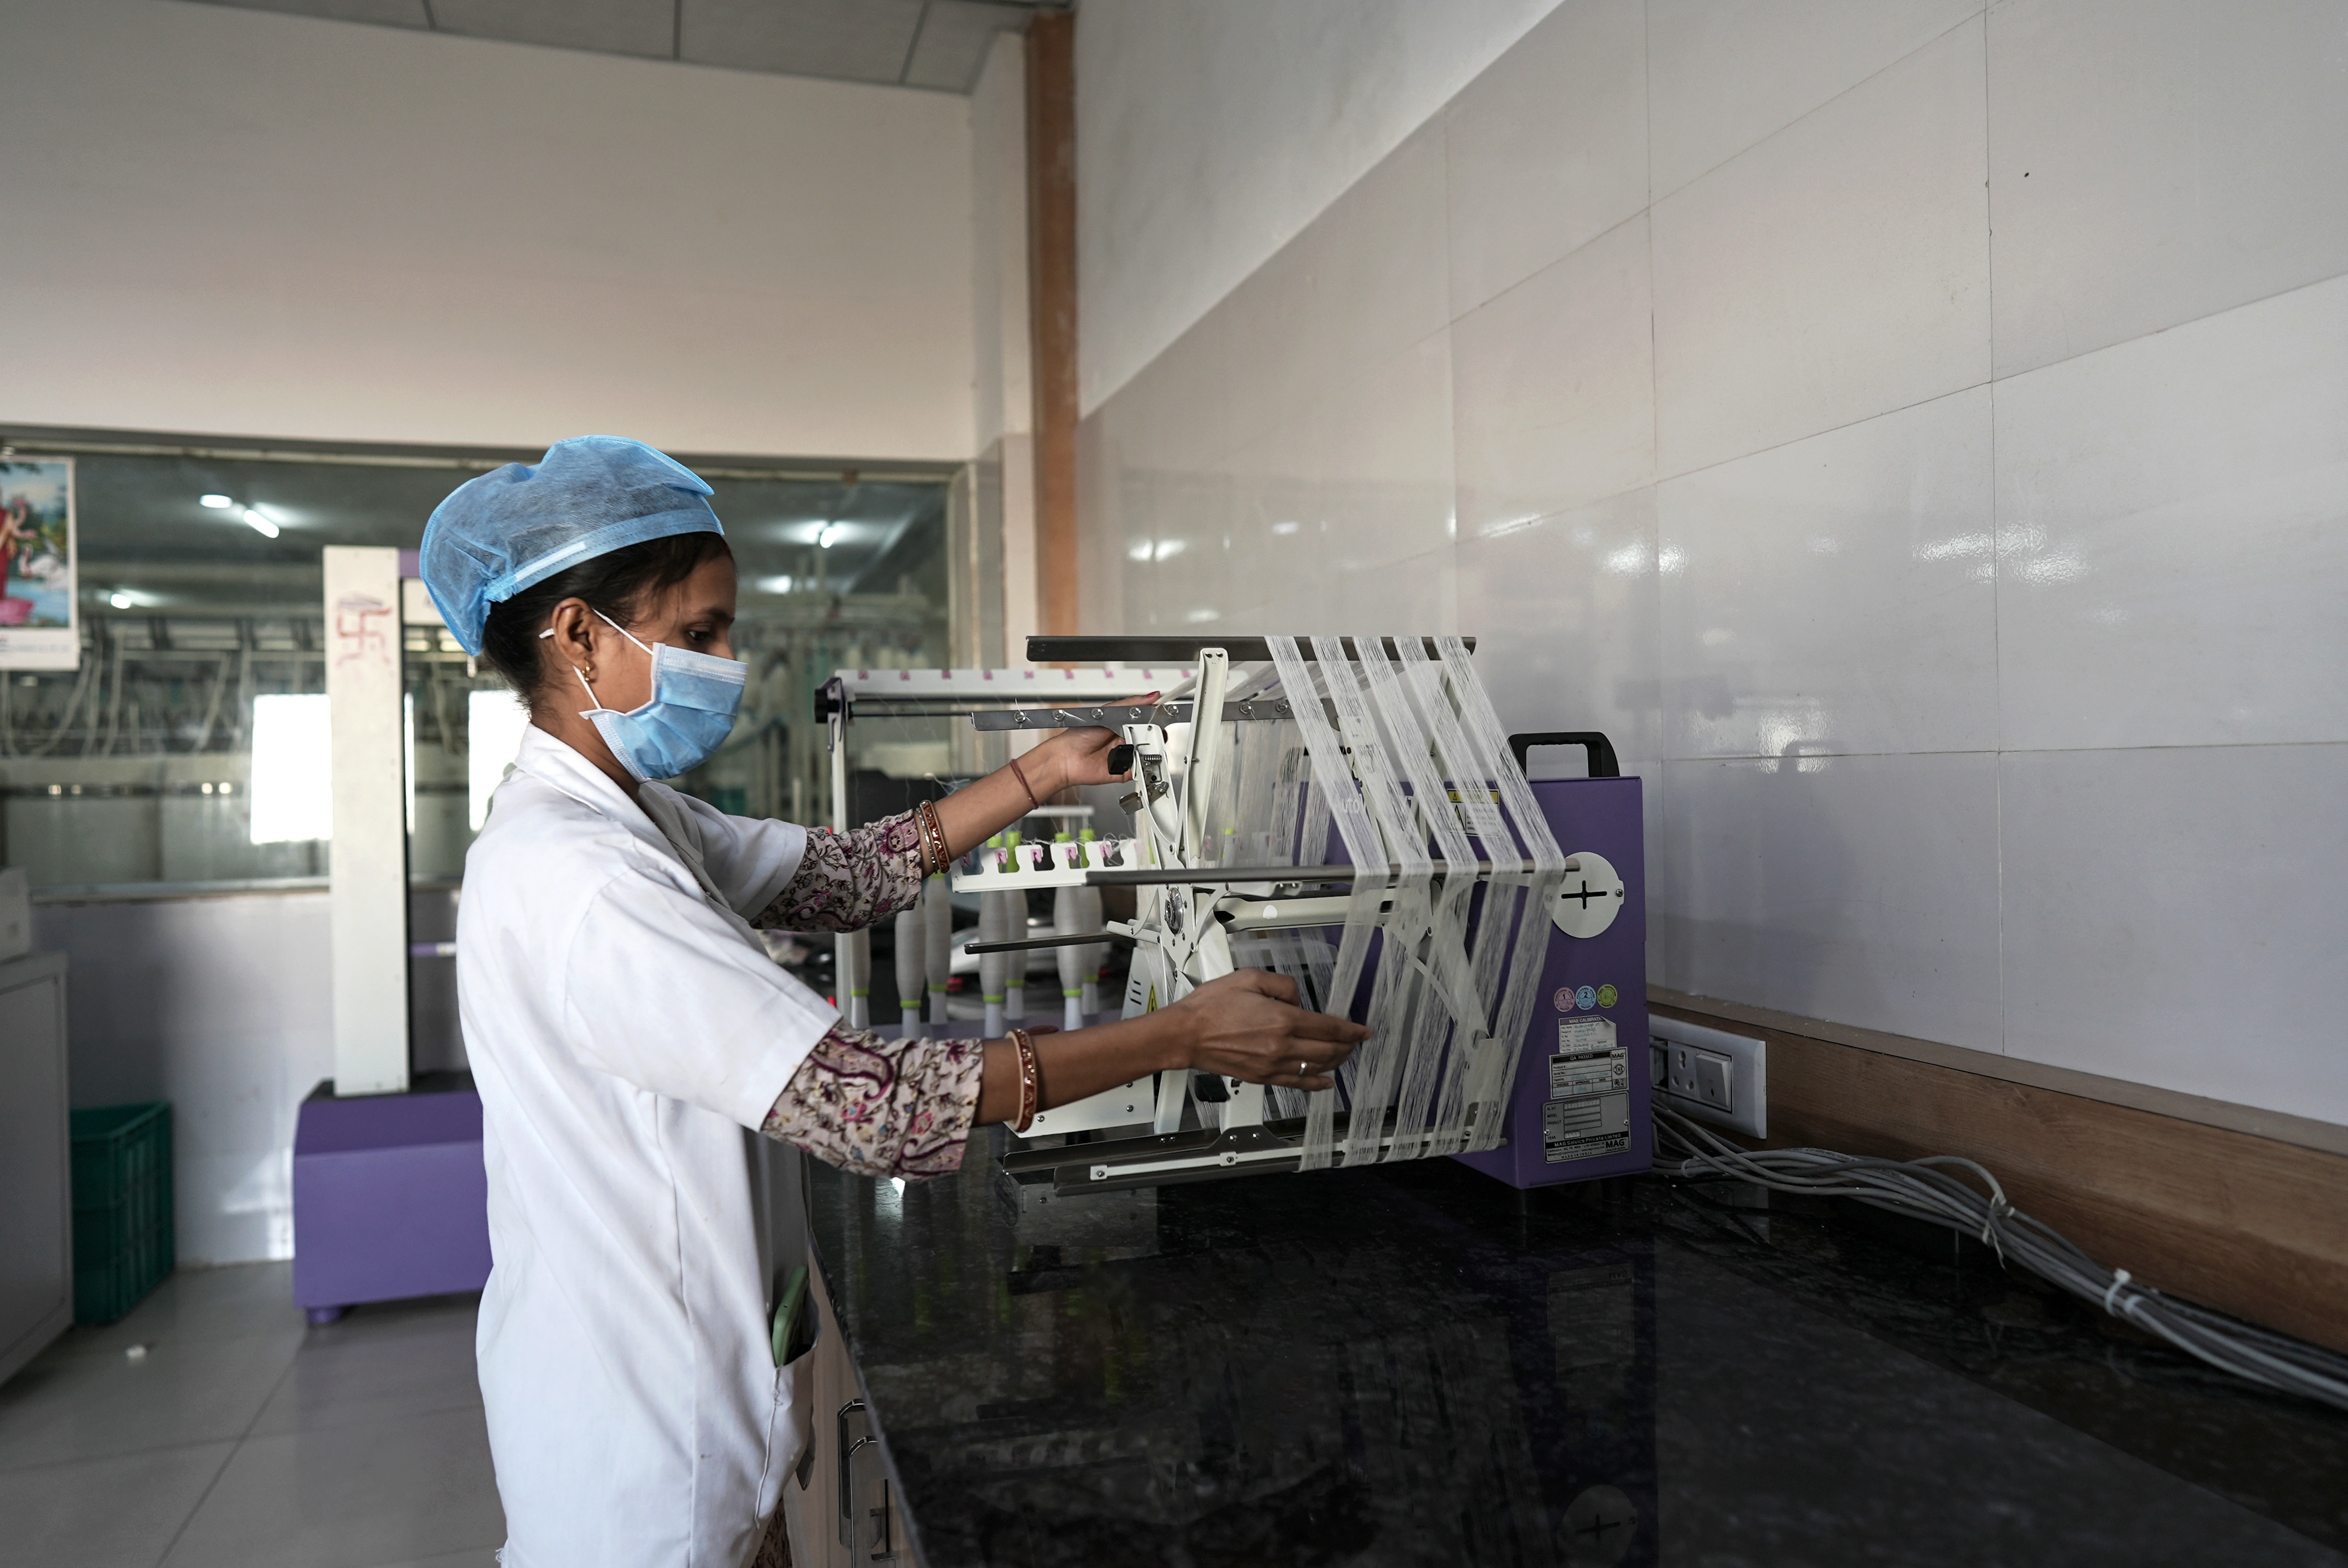
MAG Solvics Strength & Trash
Measures peak breaking load and isolates non-lint content to guarantee clean input and robust yarn tenacity.
Process Flow
4-Stage Quality Assurance Flow
Raw Cotton Testing
HVI testing for fiber staple length, micronaire fineness, and trash isolation before bale laydown.
In-Process Control
Online auto-levelers on carding, combing, and drawframes eliminate sliver count deviations.
Computerized Testing
Regular lab sampling on Premier iQ3 & MAG testers for Count, CSP, U%, and twist balance.
Clearing & Packaging
Optical yarn clearing for polypropylene elimination, UV darkroom check, and automated weighing.